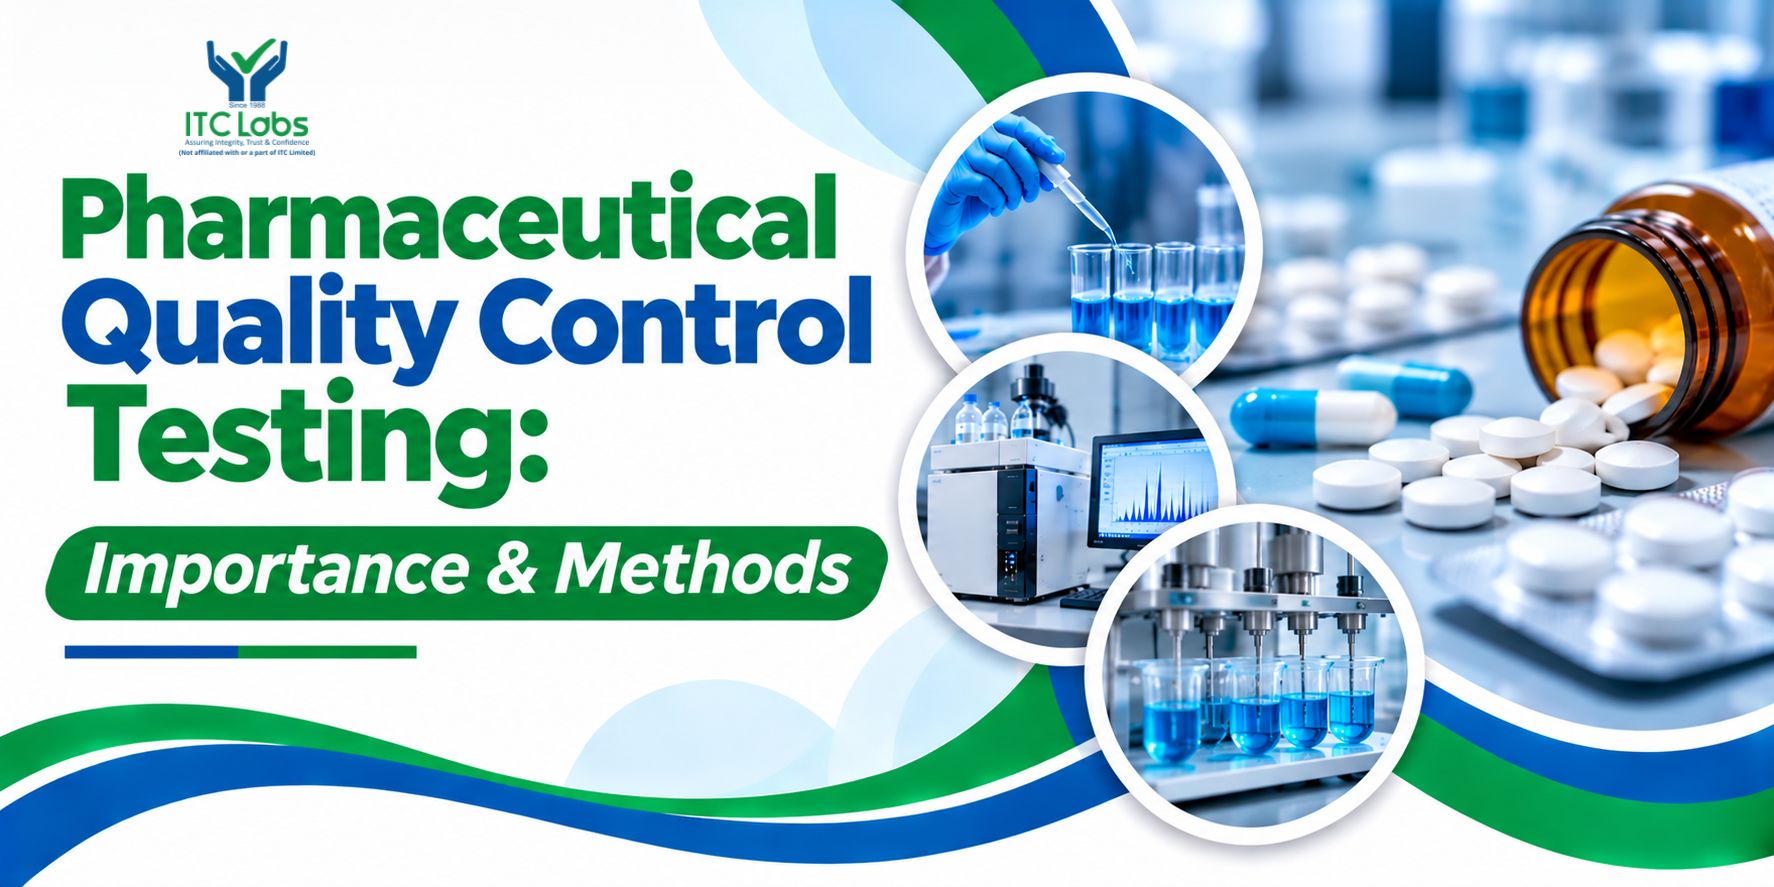
The pharmaceutical industry plays a vital role in protecting public health by developing and manufacturing medicines that help prevent, manage, and treat various health conditions. However, the effectiveness of any medicine depends on more than its formulation. It must also meet strict quality, safety, purity, and performance requirements before reaching patients.
This is where pharmaceutical quality control testing becomes essential. It involves a series of scientific tests and analytical procedures designed to verify the quality, identity, strength, purity, and safety of pharmaceutical products. From checking active pharmaceutical ingredients (APIs) to identifying harmful impurities and detecting microbial contamination, quality control testing helps ensure that medicines meet established specifications.
For pharmaceutical manufacturers, maintaining consistent product quality is essential for regulatory compliance, patient safety, and consumer confidence. Partnering with a reliable pharmaceutical testing laboratory such as Qualitek Labs can help businesses achieve these objectives through advanced analytical testing and specialised laboratory facilities.
What Is Pharmaceutical Quality Control Testing?
Pharmaceutical quality control testing refers to the systematic examination of raw materials, active pharmaceutical ingredients, intermediate products, and finished medicines to determine whether they meet predefined quality specifications.
A professional pharmaceutical testing laboratory performs different analytical and microbiological tests to evaluate product characteristics and identify potential quality issues.
These assessments help manufacturers confirm that pharmaceutical products are consistent, safe, and suitable for their intended use.
Some major areas covered under pharmaceutical quality control testing include:
- Identification and assay of active pharmaceutical ingredients.
- Chemical composition and purity analysis.
- Impurity profiling and residual solvent analysis.
- Dissolution and drug release testing.
- Elemental impurities testing.
- Microbiological contamination testing.
- Stability and shelf-life evaluation.
- Extractables and leachables studies.
These testing procedures form an important part of pharmaceutical quality assurance and help manufacturers maintain consistent product standards throughout the manufacturing process.
Why Is Pharmaceutical Quality Control Testing Important?
Quality control is essential at every stage of pharmaceutical manufacturing. Even a small variation in ingredient concentration, contamination level, or product stability can affect medicine quality and patient safety.
Here are some important reasons why pharmaceutical quality control testing is necessary.
1. Ensures Patient Safety
Patient safety is the primary objective of pharmaceutical quality control. Medicines containing harmful impurities, incorrect ingredient concentrations, or microbial contamination can create serious health risks.
Regular drug quality testing helps identify unwanted substances and potential contamination before pharmaceutical products are released into the market.
2. Verifies Drug Purity and Composition
Pharmaceutical products must contain the correct quantity of active pharmaceutical ingredients (APIs) and comply with established purity specifications.
Analytical techniques such as High-Performance Liquid Chromatography (HPLC) and Liquid Chromatography with Tandem Mass Spectrometry (LC-MS/MS) help identify and quantify chemical components and impurities.
3. Supports Regulatory Compliance
Pharmaceutical manufacturers must follow applicable national and international quality requirements.
Regular pharmaceutical compliance testing helps manufacturers demonstrate that their products meet relevant regulatory and pharmacopoeial specifications, including those outlined in:
- Indian Pharmacopoeia (IP)
- United States Pharmacopoeia (USP)
- European Pharmacopoeia (EP)
- British Pharmacopoeia (BP)
The applicable requirements depend on the product, market, and regulatory framework.
4. Maintains Product Consistency
Medicines must maintain consistent quality from one manufacturing batch to another.
Pharmaceutical quality control testing helps identify variations in chemical composition, potency, dissolution, and other quality attributes, supporting consistent manufacturing outcomes.
5. Detects Harmful Impurities
Pharmaceutical products may contain unwanted substances introduced during manufacturing, storage, or packaging.
Impurity profiling helps identify and quantify organic impurities, residual solvents, elemental impurities, and potentially harmful nitrosamine compounds.
6. Evaluates Drug Stability and Shelf Life
Medicines may undergo chemical or physical changes over time due to temperature, humidity, light, and other environmental conditions.
Stability testing helps determine how product quality changes during storage and supports the establishment of appropriate shelf-life and storage conditions.
Looking for Reliable Pharmaceutical Quality Control Testing Services?
Ensure medicine quality, purity, safety, and regulatory compliance with advanced pharmaceutical testing services from Qualitek Labs. Our expert team offers HPLC, LC-MS/MS, impurity profiling, nitrosamine testing, and microbiological testing solutions.
Major Types of Pharmaceutical Quality Control Testing
Different analytical and microbiological testing methods are used depending on the pharmaceutical formulation, manufacturing process, and regulatory requirements.
Let’s explore some important pharmaceutical testing methods.
1. HPLC Testing and Assay Analysis
High-Performance Liquid Chromatography (HPLC) is one of the most widely used analytical techniques in pharmaceutical quality control.
It separates different components of a sample and helps identify and quantify active ingredients, related substances, and impurities.
HPLC testing is commonly used for:
- Active pharmaceutical ingredient (API) assay.
- Related substances analysis.
- Impurity profiling.
- Dissolution sample analysis.
- Pharmaceutical purity assessment.
Assay testing helps determine whether a medicine contains the required concentration of its active ingredient.
Accurate HPLC analysis supports product quality, batch consistency, and regulatory compliance.
2. Dissolution Testing
Dissolution testing evaluates the rate and extent to which an active pharmaceutical ingredient is released from a dosage form under specified testing conditions.
It is particularly important for tablets and capsules because drug release characteristics can influence product performance.
The test helps manufacturers assess formulation consistency, compare batches, and evaluate whether a product meets its specified dissolution requirements.
3. Nitrosamine Impurity Testing
Nitrosamine impurities have become an important concern in pharmaceutical quality control because certain compounds in this category are classified as probable or possible human carcinogens.
These impurities may be introduced through raw materials, manufacturing processes, or other sources.
Nitrosamine testing helps identify and quantify compounds such as:
- N-Nitrosodimethylamine (NDMA).
- N-Nitrosodiethylamine (NDEA).
- N-Nitrosodiisopropylamine (NDIPA).
- N-Nitrosodi-n-butylamine (NDBA).
- N-Nitroso-N-methyl-4-aminobutyric acid (NMBA).
Advanced LC-MS/MS testing is commonly used for the sensitive identification and quantification of nitrosamine impurities in pharmaceutical products.
Regular impurity assessment helps manufacturers evaluate contamination risks and implement appropriate quality control measures.
4. Residual Solvent Analysis
Residual solvents are volatile organic chemicals that may remain in pharmaceutical products after manufacturing processes.
Some solvents can pose health risks if present above acceptable limits.
Residual solvent analysis is performed to identify and quantify these substances and determine whether their concentrations comply with applicable requirements.
Gas Chromatography (GC) and suitable mass spectrometry-based methods are commonly used for residual solvent testing.
This assessment helps pharmaceutical manufacturers maintain product purity and minimise potential safety concerns.
5. Elemental Impurities Testing
Elemental impurities may enter pharmaceutical products through raw materials, manufacturing equipment, catalysts, or environmental contamination.
Some elements can be harmful even at relatively low concentrations.
Commonly evaluated elements include:
- Lead (Pb).
- Cadmium (Cd).
- Arsenic (As).
- Mercury (Hg).
- Nickel (Ni).
- Cobalt (Co).
Analytical techniques such as Inductively Coupled Plasma Mass Spectrometry (ICP-MS), ICP-OES, and Atomic Absorption Spectroscopy (AAS) are used depending on the testing requirements.
Elemental impurities testing helps manufacturers evaluate the presence and concentration of potentially harmful elements in pharmaceutical products.
6. Pharmaceutical Microbiological Testing
Microbial contamination can compromise the quality and safety of medicines, particularly sterile pharmaceutical products.
Pharmaceutical microbiological testing evaluates the presence of microorganisms and helps determine whether products meet applicable microbiological requirements.
Important microbiological tests include:
- Microbial Limit Testing.
- Bacterial Endotoxin Testing.
- Sterility Testing.
- Preservative Efficacy Testing.
- Disinfectant Efficacy Testing.
- Growth Promotion Testing.
- Environmental Monitoring.
These assessments help manufacturers maintain appropriate microbiological quality throughout production and storage.
7. Extractables and Leachables Testing
Pharmaceutical packaging materials and manufacturing equipment may release chemical substances that can migrate into drug products.
Extractables and leachables studies help identify and assess these substances to evaluate potential risks to product quality and patient safety.
Testing may include:
- Chemical analysis.
- Organic impurity identification.
- Elemental impurity analysis.
- Assessment of potentially migrating substances.
These studies are particularly important for pharmaceutical packaging systems, medicine containers, and other product-contact materials.
8. Pharmaceutical Stability Testing
Stability testing evaluates how pharmaceutical products change over time under specified environmental conditions.
It helps determine the effects of temperature, humidity, and light on medicine quality.
Stability studies support the determination of shelf life, storage conditions, and product packaging requirements.
They are an important part of pharmaceutical product development and ongoing quality assurance.
Role of Advanced Analytical Instruments in Pharmaceutical Testing
Modern pharmaceutical testing laboratories depend on specialised analytical instruments to achieve accurate and reliable results.
Some commonly used instruments include:
| Instrument | Application |
|---|---|
| HPLC | Assay, purity, and related substances analysis |
| LC-MS/MS | Nitrosamine and trace impurity analysis |
| GC-MS/MS | Residual solvent and volatile compound analysis |
| ICP-MS | Elemental impurities testing |
| ICP-OES | Elemental composition analysis |
| AAS | Metal and elemental analysis |
These technologies help pharmaceutical manufacturers evaluate product quality using appropriate analytical methods.
However, the accuracy of results also depends on validated methods, qualified personnel, appropriate sample handling, and suitable laboratory quality systems.
Importance of Pharmacopoeial Standards in Pharmaceutical Quality Control
Pharmacopoeias provide official quality specifications and testing procedures for pharmaceutical substances and products.
Following applicable pharmacopoeial standards helps manufacturers maintain consistent product quality and meet regulatory expectations.
Some widely recognised pharmacopoeias include:
Indian Pharmacopoeia (IP): Provides official standards for pharmaceutical substances and products in India.
United States Pharmacopoeia (USP): Establishes quality standards for medicines, ingredients, and related pharmaceutical materials.
European Pharmacopoeia (EP): Provides recognised quality standards for pharmaceutical substances and preparations in Europe.
British Pharmacopoeia (BP): Contains official standards and testing requirements for pharmaceutical substances and medicinal products.
The applicable pharmacopoeia depends on the target market, product category, and regulatory requirements.
How to Choose the Right Pharmaceutical Testing Laboratory?
Choosing the right pharmaceutical testing laboratory in India is important for ensuring accurate testing results and regulatory compliance.
Before selecting a laboratory, pharmaceutical manufacturers should consider the following factors:
- Laboratory Accreditation: Verify whether the laboratory has relevant NABL accreditation and whether the required testing parameters are included in its accredited scope.
- Advanced Analytical Equipment: Ensure the laboratory has appropriate instruments such as HPLC, LC-MS/MS, GC-MS/MS, and ICP-MS for the required testing methods.
- Technical Expertise: Experienced scientists and analysts are essential for performing specialised pharmaceutical testing and interpreting results.
- Regulatory Compliance: Check whether the laboratory follows relevant IP, USP, EP, BP, and other applicable testing requirements.
- Quality Management Systems: Reliable sample handling, validated methods, documentation, and laboratory information management systems support consistent testing operations.
- Timely Reporting: Accurate and clearly documented reports help manufacturers make informed decisions about product quality and batch release.
Partnering with an experienced laboratory can strengthen pharmaceutical quality assurance and support reliable manufacturing practices.
Conclusion: Choose Qualitek Labs for Reliable Pharmaceutical Testing Services
Pharmaceutical quality control testing is essential for ensuring the safety, purity, consistency, and reliability of medicines. From HPLC assay testing and nitrosamine impurity detection to residual solvent analysis, elemental impurities testing, and microbiological assessments, comprehensive testing helps pharmaceutical manufacturers maintain product quality and meet regulatory requirements.
Selecting an experienced analytical testing partner is equally important for obtaining accurate results and maintaining confidence in pharmaceutical products.
Qualitek Labs offers comprehensive drug and pharmaceutical testing services supported by advanced analytical instruments, modern laboratory facilities, and experienced scientists and analysts.
With testing capabilities including HPLC, LC-MS/MS, GC-MS/MS, ICP-MS, microbiological testing, impurity profiling, and extractables and leachables studies, Qualitek Labs supports pharmaceutical manufacturers in addressing their analytical testing and quality control requirements.
Our commitment to accuracy, technical expertise, and regulatory alignment makes Qualitek Labs a reliable partner for pharmaceutical testing.
If you are looking for a dependable pharmaceutical testing laboratory in India, connect with Qualitek Labs for professional drug testing and pharmaceutical quality control services.
Partner with Qualitek Labs to strengthen medicine quality, ensure compliance, and support a healthier future.
Frequently Asked Questions (FAQs)
1. What is pharmaceutical quality control testing?
Pharmaceutical quality control testing involves analysing raw materials, active pharmaceutical ingredients, and finished medicines to verify their identity, purity, strength, safety, and quality. It helps manufacturers ensure that products meet applicable specifications and regulatory requirements.
2. What are the common tests performed in pharmaceutical quality control?
Common tests include HPLC assay testing, dissolution testing, impurity profiling, nitrosamine testing, residual solvent analysis, elemental impurities testing, sterility testing, microbial limit testing, and stability studies.
3. Why is HPLC testing important in pharmaceutical manufacturing?
HPLC testing helps identify and quantify active pharmaceutical ingredients, related substances, and impurities. It supports pharmaceutical purity assessment, product consistency, and quality control during manufacturing.
4. What are nitrosamine impurities, and why are they tested?
Nitrosamine impurities are chemical compounds that may occur in pharmaceutical products due to raw materials, manufacturing processes, or other contamination sources. Certain nitrosamines are classified as probable or possible human carcinogens. Testing helps manufacturers identify and quantify these impurities and evaluate compliance with applicable safety limits.
5. How do I choose a reliable pharmaceutical testing laboratory in India?
Look for a laboratory with relevant NABL accreditation, modern analytical instruments, experienced scientists, appropriate testing methodologies, and reliable reporting systems. Also verify that the laboratory’s accredited scope covers the specific tests you require.